Industrial Minerals
Coal
Overview
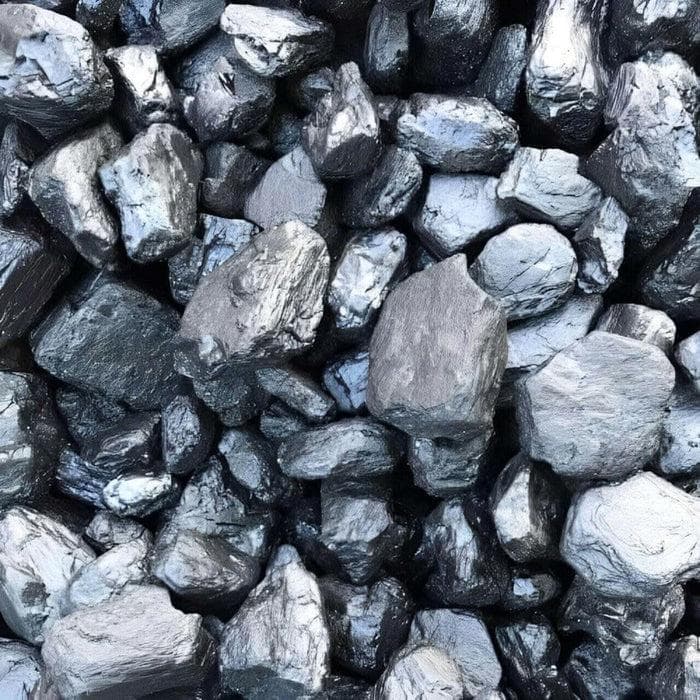
Anthracite is a premium-grade hard coal with high fixed carbon, low ash, and low volatile matter. It is widely used as a carbon additive in steelmaking, foundries, metallurgy, water filtration, and industrial heating applications.
Applications
- Steel Making
- Foundry Industry
- Carbon Additive
- Metallurgical Industry
- Water Filtration
- Power Generation
- Chemical Industry
- Industrial Heating
Chemical Composition
| Grade | FC | Ash | VM | Moisture | Sulfur |
|---|---|---|---|---|---|
| AC 85 | 85% Min | 12% Max | 6% Max | 1.0% Max | 0.5% Max |
| AC 90 | 90% Min | 8% Max | 5% Max | 1.0% Max | 0.4% Max |
| AC 95 | 95% Min | 5% Max | 3% Max | 0.8% Max | 0.3% Max |
Physical Properties
| Property | Value |
|---|---|
| Appearance | Black |
| Shape | Lumps |
| Color | Black |
| Density | 1.4–1.6 g/cm³ |
| SpecificGravity | 1.5 |
| CalorificValue | 7000–8500 Kcal/kg |
| Packing | 25 Kg Bags / 1 MT Jumbo Bag |
| Storage | StoreDryCoveredArea |
Frequently Asked Questions
Anthracite is the highest-grade natural coal with high carbon content, low sulfur, and low volatile matter. It is widely used as a carbon additive, fuel, and filtration media in industrial applications.